Custom Projector Heat Sink Manufacturing
Engineering teams developing projectors need heat sinks that remove concentrated heat from LED or lamp sources while fitting tight chassis dimensions. We evaluate your heat load, airflow path, and space limits, then select the manufacturing route that meets both thermal targets and unit cost.
What You Receive When You Submit a Project
-
A DFM report within days that flags fin density limits, mounting hole positions, and material options before any tooling is cut.
-
Prototype parts produced on the same skiving or extrusion lines used for later volume runs, so test results translate directly to production.
-
Thermal resistance data measured on your exact heat source size and airflow condition, not generic catalog values.
-
A single supply chain that moves from prototype validation to pilot run without requalifying a new vendor.
Manufacturing Routes Matched to Projector Requirements
Each projector platform has unique thermal and mechanical constraints. We select the optimal manufacturing process based on your heat load, form factor, and volume.
Skived Fin Heat Sinks
Deliver high surface area in compact footprints common to portable and short-throw projectors.
Extruded Profiles with CNC
Provide repeatable mounting features at higher volumes with secondary machining operations.
Cold Forged Pin-Fin Designs
Suit round LED arrays where omnidirectional airflow is available.
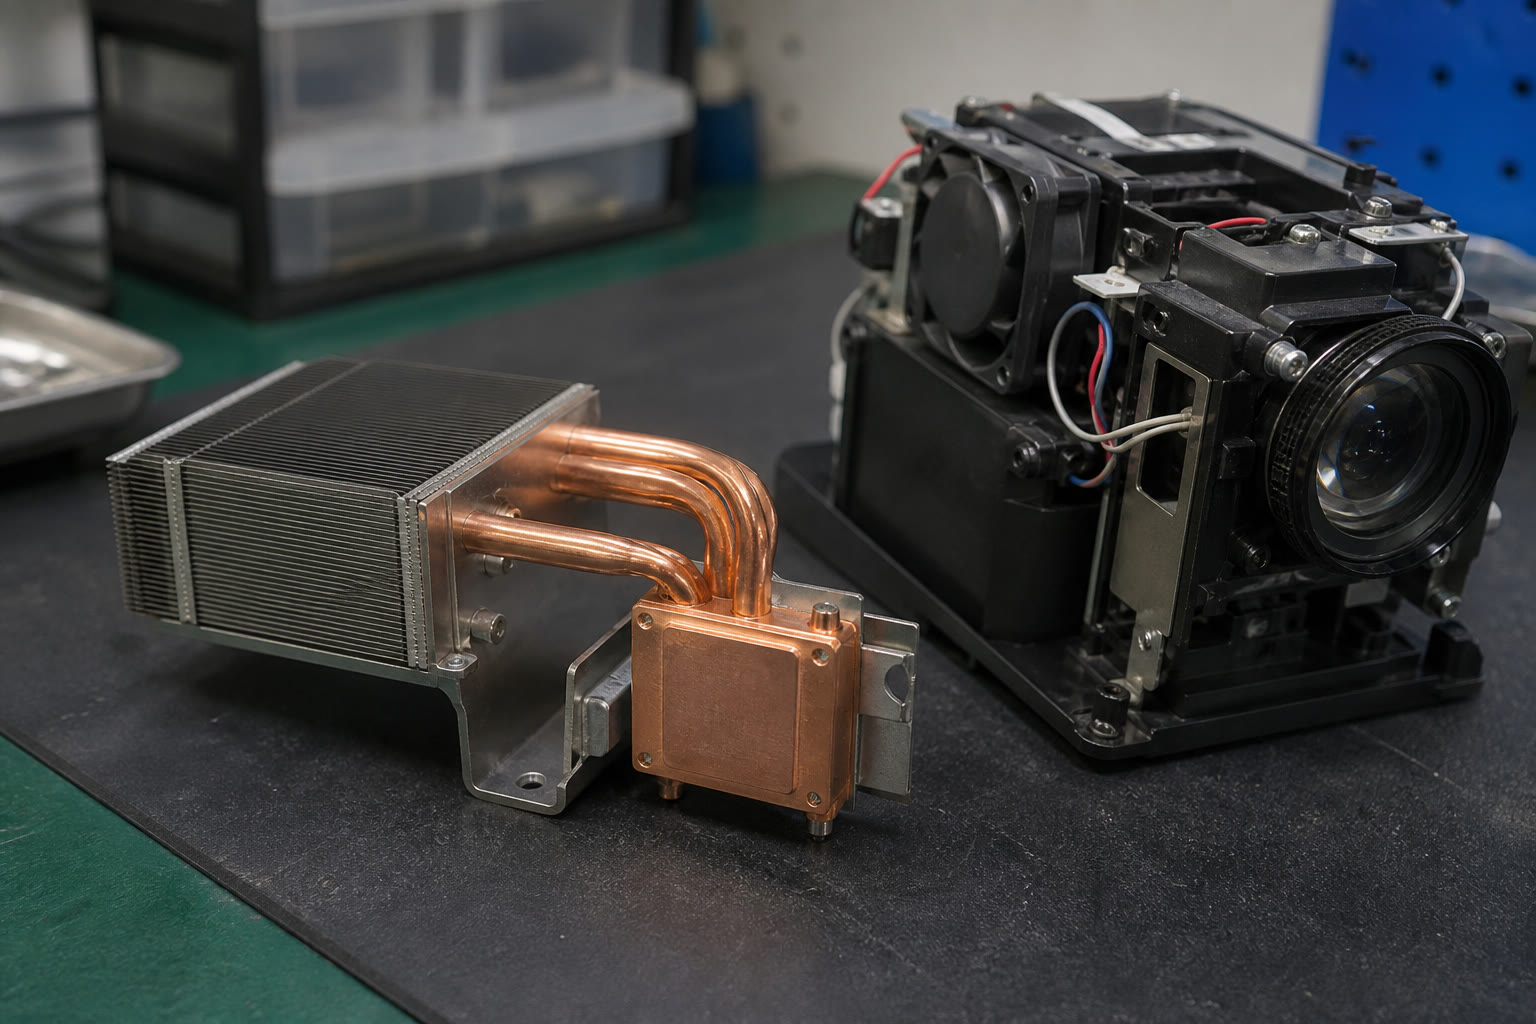
Heat Pipe Assemblies
Spread heat from a small die to larger dissipation areas when chassis airflow is limited.
Skived Fin Capability for Projector Applications
These ranges allow fin densities that standard extrusion cannot achieve, directly lowering thermal resistance for the same footprint.
Upload Your Drawing| Parameter | Range |
|---|---|
| Base thickness | 1–40 mm |
| Fin height | up to 140 mm |
| Fin thickness | 0.05–2.0 mm |
| Fin gap | 0.05–10 mm |
| Overall length | up to 2000 mm |
Extrusion and Secondary Machining
We run 800–5000 ton presses on 6063 and 6061 aluminum, then add milling, drilling, and tapping in-house. High-aspect-ratio fins above 20:1 are possible on suitable profiles.
When width exceeds single-extrusion limits, friction-stir-welded assemblies reach up to 762 mm while maintaining structural integrity.
How Short Lead Times Reduce Your Project Risk
A validated prototype in weeks lets you complete thermal chamber testing and mechanical fit checks early.
Early data confirms whether the chosen process meets both performance and cost targets, avoiding late-stage redesigns that delay market launch.
Typical Data Needed for an RFQ
Send any of the following and we return a preliminary process recommendation and budget range:
2D or 3D Files
Heat Load & Source Dimensions
Max Temperature & Ambient
Available Airflow (CFM)
Annual Volume Estimate
Request a DFM Discussion
Reply with your projector thermal requirements and we will schedule a DFM discussion.