Custom Die-Cast Heat Sinks for High-Power Electronics
We design and manufacture custom die-cast heat sinks and thermal assemblies from prototype to mass production.
Our engineering team turns thermal requirements, 2D and 3D drawings, and product concepts into manufacturable die-cast heat sinks and integrated cooling solutions. We support OEMs and equipment manufacturers worldwide with DFM, tooling, prototyping, CNC finishing, thermal testing, and volume production.
2014
Engineering support established
End-to-end
DFM through production
Engineering-first
Thermal, mechanical, and manufacturability review.
Multi-process
Die casting, machining, finishing, and hybrid cooling.
Production-ready
Validation, quality control, and volume supply.
What we deliver
A complete die-cast thermal assembly supply chain
We combine multiple thermal manufacturing technologies under one supply chain. If die casting is the right path, we take it. If another process is a better fit, we recommend and manufacture it.
Custom die-cast components
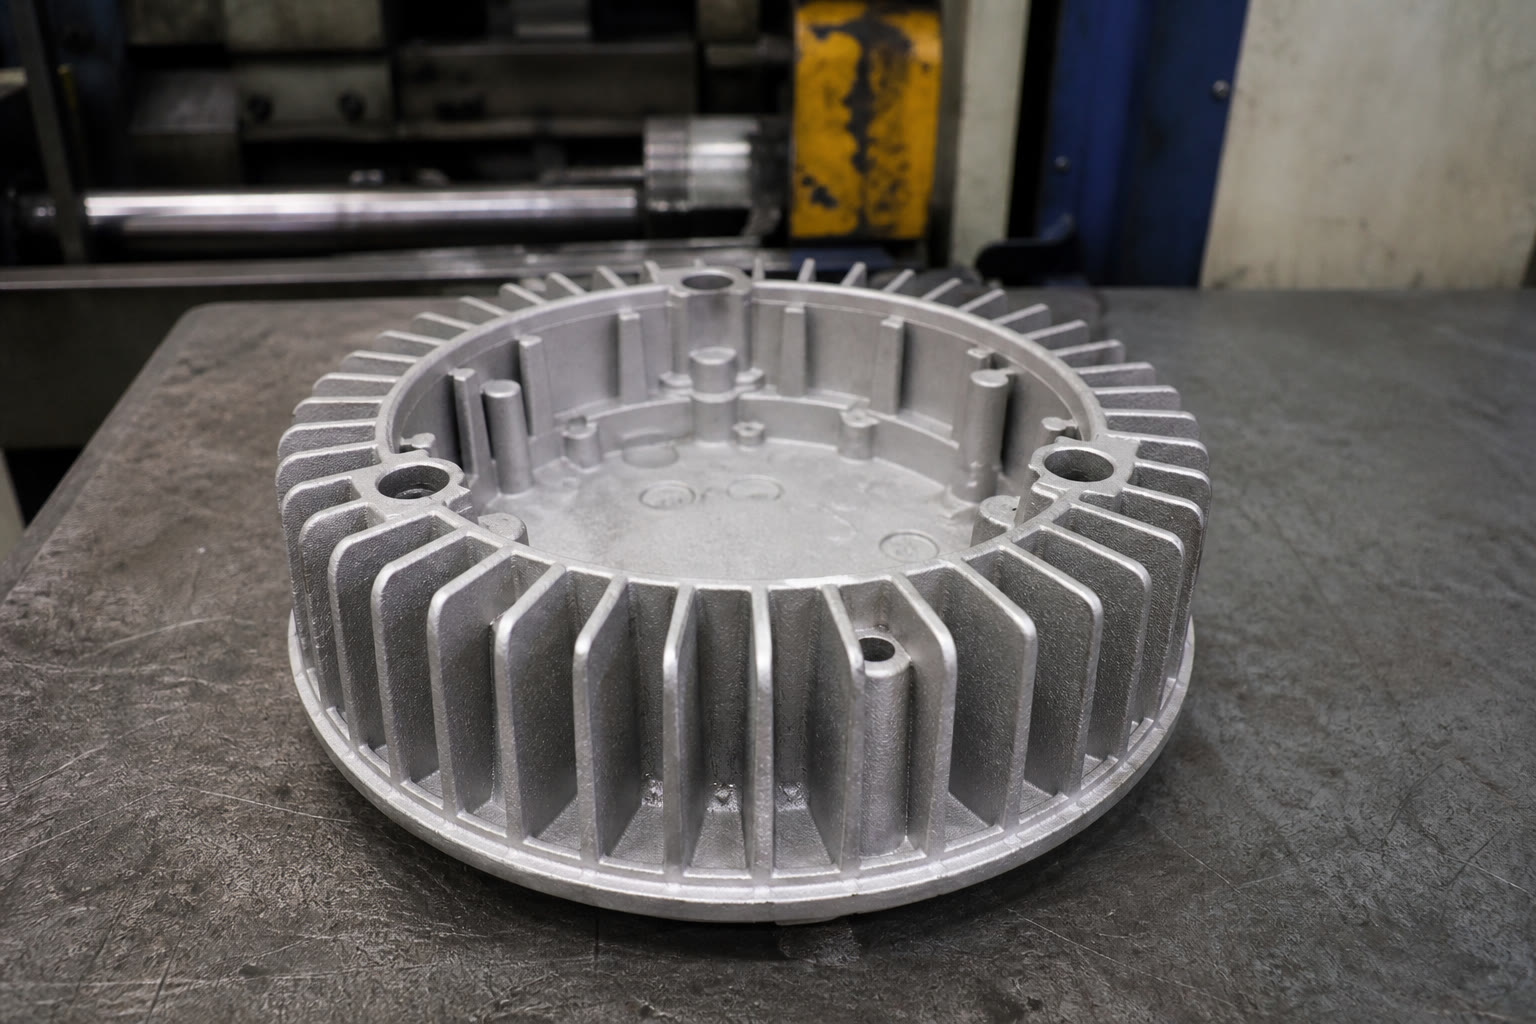
Aluminum heat sinks, heat sink housings, integrated bosses, ribs, cored airflow paths, and cable or connector provisions.
Higher-performance assemblies
Die-cast bases with skived or bonded fins, embedded heat pipes, internal modules, or integrated liquid cold plates.
Machining and surface treatment
CNC milling, drilling, tapping, turning, flatness control, anodizing, hard anodizing, nickel plating, passivation, polishing, and cleaning.
Measured thermal performance
Dimensional inspection, CMM measurement, thermal resistance testing, and leakage testing for liquid circuits where applicable.
From concept to T1
Prototype development, optimization, tooling coordination, casting trials, CNC finishing, and sample approval support.
Volume production control
Qualified partner foundries under our engineering and quality control, followed by in-house precision machining, finishing, and assembly.
Process selection
When is die casting the right choice?
Die casting is a strong option for complex geometry, medium to high volumes, integrated features, and consistent near-net shapes before CNC finishing.
- ●Integrated housings, ducts, mounting bosses, and cored airflow paths
- ●Tooling economics that support medium and high production volumes
- ●Reduced part count through cast-in structural and assembly features
- ●Repeatable near-net shapes with post-machined critical surfaces
Important tradeoffs
- Cast alloys generally have lower thermal conductivity than wrought 6xxx extrusion alloys.
- Minimum fin thickness and draft angles limit fin density.
- Porosity control and interface flatness may require post-machining.
- Ultra-high fin density or extreme aspect ratios may be better served by skived, extruded, cold-forged, brazed, or liquid-cooled designs.
Engineering-led DFM
Design for thermal performance and repeatable production
Our thermal and mechanical engineers collaborate with your team to make the design manufacturable, efficient, and ready for scale.
Typical DFM priorities
Smooth transitions, controlled wall thickness, ribs for stiffness, draft for ejection, radii for metal flow, and planned machining allowances on critical interfaces.
Thermal development
Thermal solution development, simulation support, heat sink structure, and mechanical design.
Process selection
Material and process selection across die casting, skiving, extrusion, cold forging, brazing, and liquid cooling.
Prototype optimization
Prototype development, validation, thermal resistance testing, and design optimization.
Manufacturability review
Detailed review of casting geometry, tolerances, tooling strategy, machining, and assembly requirements.
Technical reference
Typical die-cast specifications
Final specifications depend on geometry, alloy, tooling, thermal targets, and required finishing.
| Alloys | ADC12 (A383), A380, AlSi9Cu3; others upon evaluation |
|---|---|
| Fin and wall guidelines | Minimum fin thickness typically 1.5–2.5 mm; draft angle typically 0.5–2.0°; as-cast fin aspect ratio often up to approximately 8–12:1 |
| As-cast features | Integrated bosses, ribs, cored channels, logo marking, and cable or connector provisions |
| Post-machining | CNC milling, drilling, tapping, turning, flatness and roughness control; typical machined feature tolerance to ±0.02 mm, with machine capability of ±0.002–±0.008 mm |
| Finishing | Anodizing, hard anodizing, nickel plating, passivation, sandblasting, polishing, and cleaning |
| Inspection | CMM, 2D measurement, dimensional inspection, thermal testing, and leakage or pressure testing for liquid-cooled assemblies |
Hybrid and advanced thermal options
Balance thermal performance, structure, volume, and cost
When die casting alone cannot meet your thermal target, we integrate additional processes into a production-ready assembly.
Die-cast base plus skived or bonded fins
Adds surface area where as-cast fin density is not sufficient.
Embedded heat pipes
Spreads hotspot loads through a die-cast base or housing.
Internal heat sink modules
Integrates extruded or cold-forged structures inside a die-cast enclosure.
Liquid cold plate integration
Supports high heat flux applications beyond the practical range of air cooling.
Quality assurance
Validation built into the production path
- ✓Dimensional and CMM inspection against drawings and GD&T
- ✓Thermal resistance testing to verify design assumptions
- ✓Surface flatness and roughness control at thermal interfaces
- ✓Leakage and pressure testing for liquid-cooled variants
- ✓Material, coating, and finish verification as specified
PPAP- or APQP-style documentation is available upon request for regulated industries.
Industries served
Thermal solutions for demanding equipment
From RFQ to production
A clear path from prototype to mass production
Prototype → Validation → Pilot Run → Mass Production
RFQ and DFM
Review drawings, thermal targets, materials, tolerances, and production requirements.
3–7 working days
Tooling and trials
Develop tooling, cast trial parts, and coordinate CNC finishing and validation.
Typically 4–8 weeks
T1 and pilot run
Deliver samples, complete approval activities, and confirm production readiness.
T1 in 1–2 weeks after trial
Mass production
Schedule releases against your capacity plan and annual volume requirements.
Pilot in 2–4 weeks after approval
Design for cost
What influences the final cost?
- Tool complexity and cavity count
- Alloy selection and shot weight
- Fin thickness, draft, ribs, and cored features
- Machining operations and tolerances
- Surface finish and coating requirements
- Thermal target, pressure drop, and annual volume
Our recommendations
Make the design efficient before tooling
- 01Consolidate features in the casting to reduce secondary assembly.
- 02Use consistent wall thickness where possible.
- 03Reserve tight tolerances for key machined areas rather than the full casting.
- 04Use hybrid fin solutions where the thermal gain justifies added steps.
Mini case snapshots
Production-focused solutions across applications
Power inverter housing
Die-cast aluminum enclosure with cored airflow, CNC-machined interface pads, and black anodized finish. Embedded heat pipes spread hotspot loads while reducing assembly count.
Industrial drive module
Die-cast base with bonded fin array for increased surface area. Delivered cost reduction versus a fully machined block while meeting flatness and thermal specifications.
Telecom equipment
Die-cast heat sink with integrated mounting bosses and cable channels, moving from T1 to mass production with anodized finish and full dimensional validation.
Ready to quote
Let’s review your die-cast heat sink design
Send us your drawing and requirements. We’ll review thermal targets, DFM, and manufacturability, then recommend the most suitable path and provide a clear quotation and timeline.
RFQ checklist
- 2D drawing and 3D CAD file
- Heat load and temperature limits
- Airflow or coolant conditions
- Envelope and mounting constraints
- Finish and tolerance requirements
- Annual volume and ramp schedule
Talk to a thermal engineer
Share your project details and our team will help identify the most practical production route.
HeatsinkMaker — Custom Thermal Solutions.
Built for production.